


The plastics and composites manufacturing industry uses a range of processing machines, each suited to different materials, geometries, and production volumes. Understanding how these processes differ — and where each performs best — is essential for engineers and procurement managers selecting equipment or specifying manufacturing methods for structural and industrial components. This article covers the major plastic and composite machinery categories, with particular focus on pultrusion machines and how they compare to injection molding, extrusion, blow molding, and compression molding equipment.
Pultrusion Machines
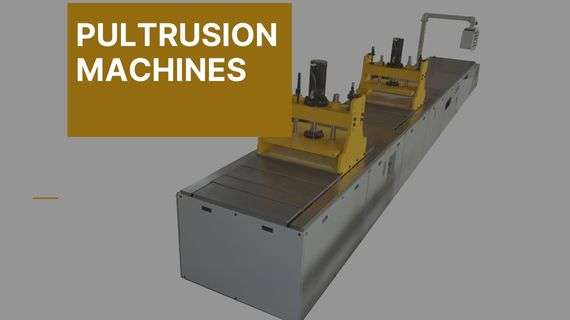
Pultrusion machines produce continuous fiber-reinforced polymer (FRP) composite profiles with constant cross-section geometry. The process pulls glass, carbon, or aramid fiber reinforcements through a liquid resin bath for full impregnation, then through a heated die that simultaneously shapes the profile and cures the resin. The result is a continuous composite profile that is cut to length by an automated saw downstream of the puller.
The key components of a pultrusion line are the fiber creel system, resin bath or closed injection system, preformer and guide plate assembly, heated die, pulling mechanism, and cut-off saw. The fiber creel holds spools of reinforcing fiber at controlled tension; the preformer organizes the fiber architecture into the correct spatial arrangement before the material enters the die; the heated die — typically 900–1100 mm long with 4–6 independently controlled temperature zones at 120–170°C — shapes and cures the composite; and the pulling mechanism — either a reciprocating gripper puller or caterpillar puller — draws the cured profile through the machine at controlled speed.
Production speeds for standard glass fiber profiles in polyester or vinyl ester resin are typically 0.5–2.0 m/min, with fiber volume fractions of 55–65% achievable under controlled process conditions. Dimensional tolerances of ±0.3–0.5 mm on profile cross-section dimensions are standard in production.
Pultrusion machines are used to produce structural profiles for construction and civil infrastructure — beams, angles, channels, I-sections, flat bar, rod, and tube — as well as electrical utility poles and crossarms, FRP rebar for concrete reinforcement, cable trays, gratings, handrails, and industrial structural shapes for chemical processing and marine environments. The combination of continuous production, high fiber volume fraction, corrosion resistance, and consistent mechanical properties makes pultrusion the preferred process for long structural FRP profiles in volume production.
Injection Molding Machines

Injection molding machines produce discrete plastic parts by injecting molten thermoplastic or thermoset resin under high pressure into a closed mold cavity. The process consists of four stages: plasticization of plastic pellets in a heated barrel by a rotating screw; injection of the melt into the mold at pressures typically ranging from 70–200 MPa; cooling and solidification in the mold; and ejection of the finished part.
The process is highly automated and cyclic, with cycle times ranging from a few seconds for small thin-wall parts to several minutes for large thick-section components. Injection molding is the dominant manufacturing method for high-volume production of complex three-dimensional plastic parts — automotive interior components, electronic device housings, medical disposables, consumer product packaging, and appliance parts.
Injection molding machines are classified by drive system (hydraulic, all-electric, or hybrid), by clamping force (from less than 10 tonnes for small parts to over 5,000 tonnes for large automotive components), and by screw configuration (standard three-zone, barrier, or mixing screw designs suited to different material and quality requirements).
The key distinction from pultrusion is geometry and material: injection molding excels at complex three-dimensional discrete parts in unreinforced or short-fiber thermoplastics; pultrusion excels at continuous constant-cross-section profiles in long-fiber or continuous-fiber thermoset composites with substantially higher structural performance.
Extruders

Plastic extruders produce continuous profiles, pipes, sheets, and films by melting thermoplastic resin in a heated barrel using a rotating screw and forcing the melt through a shaping die. Unlike pultrusion — which uses thermoset resins that cure chemically and irreversibly in the die — extrusion processes thermoplastic materials that solidify on cooling and can in principle be remelted.
Single-screw extruders are the most common configuration, suitable for most thermoplastic pipe, profile, sheet, and film applications. Twin-screw extruders — either co-rotating or counter-rotating — provide better mixing and are used for compounding, highly filled materials, reactive extrusion, and processing of materials requiring intensive distributive mixing such as wood-plastic composites and filled engineering polymers.
Extruded products include PVC and HDPE pipe, window and door profiles, polyolefin and PVC sheet, packaging film, wire and cable insulation, and thermoplastic structural profiles. Thermoplastic extruded profiles and pultruded FRP profiles are sometimes direct competitors in structural applications — window and door profiles, for example, are available in both PVC extrusion and FRP pultrusion — with FRP offering superior stiffness-to-weight ratio and UV resistance at higher cost, and PVC offering lower cost and established recycling infrastructure.
Blow Molding Machines
Blow molding machines produce hollow plastic parts by inflating a softened plastic preform inside a closed mold using compressed air. The two primary variants are extrusion blow molding — where a continuous extruded parison is clamped and inflated — and injection blow molding, where an injection-molded preform is transferred to a blow station and inflated. Stretch blow molding, used for PET beverage bottles, adds biaxial stretching to the inflation step to improve mechanical properties and clarity.
Blow molding is the standard process for beverage bottles, containers, automotive fuel tanks, industrial drums, and medical fluid bags — applications requiring hollow geometry with controlled wall thickness that cannot be achieved by injection molding or extrusion. It has no direct overlap with pultrusion, as the two processes address entirely different part geometries and material systems.
Compression Molding Machines
Compression molding applies heat and pressure to thermoset materials or fiber-reinforced composites placed in an open mold, causing the material to flow and cure under the applied conditions. The process is used for Sheet Molding Compound (SMC) and Bulk Molding Compound (BMC) automotive body panels and structural parts, as well as for thermoset electrical components, rubber parts, and carbon fiber composite structural elements in aerospace and high-performance automotive applications.
Compression molding shares material territory with pultrusion — both process thermoset fiber-reinforced composites — but addresses different geometries. Compression molding produces discrete three-dimensional parts with variable cross-section and surface detail on both faces; pultrusion produces continuous constant-cross-section profiles. For structural composite parts with complex three-dimensional geometry, compression molding or resin transfer molding is specified; for long structural members with consistent cross-section, pultrusion is more economical and produces better fiber alignment and higher fiber volume fraction.
Process Comparison
The table below summarizes the key characteristics of each manufacturing process for selecting the appropriate technology for a given application:
| Process | Material Type | Part Geometry | Production Rate | Fiber Volume Fraction | Best Application |
|---|---|---|---|---|---|
| Pultrusion | Thermoset FRP (continuous fiber) | Constant cross-section profiles | 0.5–2.0 m/min continuous | 55–65% | Structural FRP profiles, rebar, utility poles |
| Injection molding | Thermoplastic (unreinforced or short fiber) | Complex 3D discrete parts | Seconds to minutes per cycle | 10–30% (short fiber) | High-volume complex parts: automotive, electronics, consumer goods |
| Extrusion | Thermoplastic | Continuous profiles, pipe, sheet, film | High continuous output | N/A (typically unreinforced) | Pipe, window profiles, packaging film |
| Blow molding | Thermoplastic | Hollow discrete parts | High volume cyclic | N/A | Bottles, containers, fuel tanks |
| Compression molding | Thermoset or FRP (SMC/BMC) | Complex 3D panels and parts | Minutes per cycle | 20–45% (SMC) | Automotive body panels, composite structural parts |
The most significant distinction between pultrusion and the thermoplastic processes (injection molding, extrusion, blow molding) is fiber architecture and resulting mechanical performance. Pultrusion achieves continuous fiber reinforcement at 55–65% volume fraction with controlled fiber orientation, producing structural composite profiles with tensile strength of 200–500 MPa for glass fiber systems and substantially higher for carbon fiber. Injection-molded short-fiber composites at 10–30% fiber volume fraction produce tensile strengths of 80–180 MPa depending on material and fiber length — adequate for many structural applications but significantly below the performance achievable in pultruded profiles under equivalent loading.
Frequently Asked Questions
What is the difference between pultrusion and extrusion?
Pultrusion and extrusion both produce continuous profiles with constant cross-section, but they process fundamentally different materials by different mechanisms. Extrusion melts thermoplastic resin using a rotating screw and forces it through a shaping die, producing profiles that solidify on cooling and can be remelted. Pultrusion pulls continuous fiber reinforcements through a thermoset resin bath and then through a heated die where chemical cure takes place, producing a composite profile that cannot be remelted. Pultruded FRP profiles have substantially higher tensile strength, stiffness-to-weight ratio, and corrosion resistance than thermoplastic extruded profiles of equivalent cross-section, at higher material cost.
What types of profiles can pultrusion machines produce?
Pultrusion machines produce any constant cross-section profile that can be formed through a die and pulled continuously: solid rod and bar, round and square tube, flat bar and plate, angle sections, channel sections, I-beams, H-sections, T-profiles, and custom complex shapes. Profile dimensions range from small-diameter rods under 10 mm to wide structural sections exceeding 500 mm. The constraint is that cross-section must be constant along the full length — variable cross-section geometry requires different manufacturing processes such as compression molding or resin transfer molding.
How does pultrusion compare to injection molding for structural composite parts?
Pultrusion and injection molding address different structural applications. Pultrusion uses continuous fiber reinforcement at 55–65% fiber volume fraction and produces profiles with tensile strength of 200–500 MPa for glass fiber systems — suitable for primary structural members in construction, infrastructure, and industrial applications. Injection molding typically uses short chopped fibers at 10–30% volume fraction, producing tensile strengths of 80–180 MPa — suitable for structural housings, brackets, and complex-geometry components where continuous fiber cannot be accommodated. For long linear structural members under bending or axial load, pultrusion is the appropriate process; for complex three-dimensional discrete structural parts, injection molding or compression molding is specified.
What materials are processed by pultrusion machines?
Pultrusion processes thermoset resin systems — most commonly unsaturated polyester, vinyl ester, epoxy, and polyurethane — combined with glass, carbon, or aramid fiber reinforcements. Polyester is the most widely used resin for cost-sensitive structural profiles. Vinyl ester is specified for chemical resistance applications. Epoxy is used for highest mechanical performance. Polyurethane pultrusion systems are adopted where high toughness and impact resistance are required. Glass fiber (E-glass or ECR-glass) is the standard reinforcement for construction and industrial profiles; carbon fiber is used where maximum stiffness-to-weight ratio justifies the cost premium.
What production speed does a pultrusion machine achieve?
Standard pultrusion production speeds for glass fiber profiles in polyester or vinyl ester resin are 0.5–2.0 m/min, depending on profile cross-section complexity, wall thickness, and resin cure kinetics. Thin solid-section profiles with fast-cure resin systems achieve the higher end of this range; thick-section or complex profiles with slower resin systems require reduced speed to ensure complete through-cure before the profile exits the die. Production speed is a primary economic parameter in pultrusion — higher speed reduces cost per meter but must be balanced against cure completeness and profile quality.
When should compression molding be used instead of pultrusion for FRP parts?
Compression molding is the appropriate choice when the FRP part requires variable cross-section geometry, complex three-dimensional shape, or surface detail on both faces that pultrusion’s constant cross-section constraint cannot accommodate. Automotive body panels, curved structural panels, and complex brackets are typical compression molding applications. Pultrusion is preferred when the part is a long profile with constant cross-section and the application requires the higher fiber volume fraction and better fiber alignment that continuous fiber pultrusion achieves relative to the chopped or woven mat reinforcements used in SMC compression molding. Where both processes are technically feasible, pultrusion is typically more economical for long profiles in volume production due to its continuous output rate.
Request a B2B Manufacturing Quote – Share your profile, rebar, machine, or die requirements and we will return specifications, lead time, and export pricing. Contact IncomePultrusion for a project quote.

